


Home Products Labels & supplies Labels BRCGS certificate
BRC
Certified packaging
High product safety
The BRCGS certificate guarantees strict standards for hygiene and quality in the production of packaging materials.
International recognition
Globally recognised standard for labels and packaging, accepted by retailers and the food industry.
Reliable traceability
Full control and traceability throughout the entire production chain.
Information
The BRCGS Global Standard Packaging Materials is a leading international standard for product safety, hygiene and quality management in the production of packaging materials and labels. Codipack is certified to this standard. This means our production processes are audited annually by an independent body, covering areas such as hygiene, process control, traceability and risk management.
For you as a customer, this provides concrete assurance: the labels you purchase from Codipack are produced under controlled and hygienic conditions and meet the requirements that retailers and the food industry impose on their suppliers. This minimises the risk of contamination and allows you to demonstrably comply with the requirements of your own customers and regulations — without any additional audit burden on your side.
Show more
- Standard: BRCGS Global Standard Packaging Materials (Issue 7)
- Focus areas: product safety, hygiene, quality management and risk analysis (HARA)
- Audit frequency: annual audit by an independent certification body
- Audit result: grade AA (2026)
- Scope: production of labels and packaging materials, including for the food industry
- Traceability: full batch and material traceability
- Certificate validity: 12 months, renewed annually
- Certified since: 2017
Frequently asked questions
Coding and labeling is our core business. We have 5000 customers in very diverse sectors: from the cheese shop around the corner to the multinational.
What is the purpose of the BRC certificate?
It ensures food safety and quality in packaging production through strict hygiene and process control protocols.
In which applications is it used?
Primarily in label and packaging production for the food industry.
How is certification achieved?
Through annual audits by accredited bodies based on BRC criteria.
What are the traceability benefits?
Requires full documentation of materials and batches for rapid traceability.
Others also viewed

Zebra VC8300
Ultra-rugged forklift computer
Designed for extreme environments with IP66 protection and operation from approximately -30°C to 50°C.
Seamless Android migration for TE apps
Runs existing terminal emulation apps directly and converts green screens to touch apps with All-Touch Terminal Emulation.
Excellent readability and operation
8″ WXGA touchscreen with approximately 1000 nits, suitable for glove use, and integrated keyboard in one compact housing.

Epson ColorWorks C8000
Ultra-high print speed
Up to 300 mm/s full-color printing, comparable to monochrome thermal printers.
Permanent printhead
No replacement needed up to 500 km print capacity for low maintenance costs.
On-demand labeling solution
Eliminates pre-print costs, inventory, and waste with high-capacity ink.
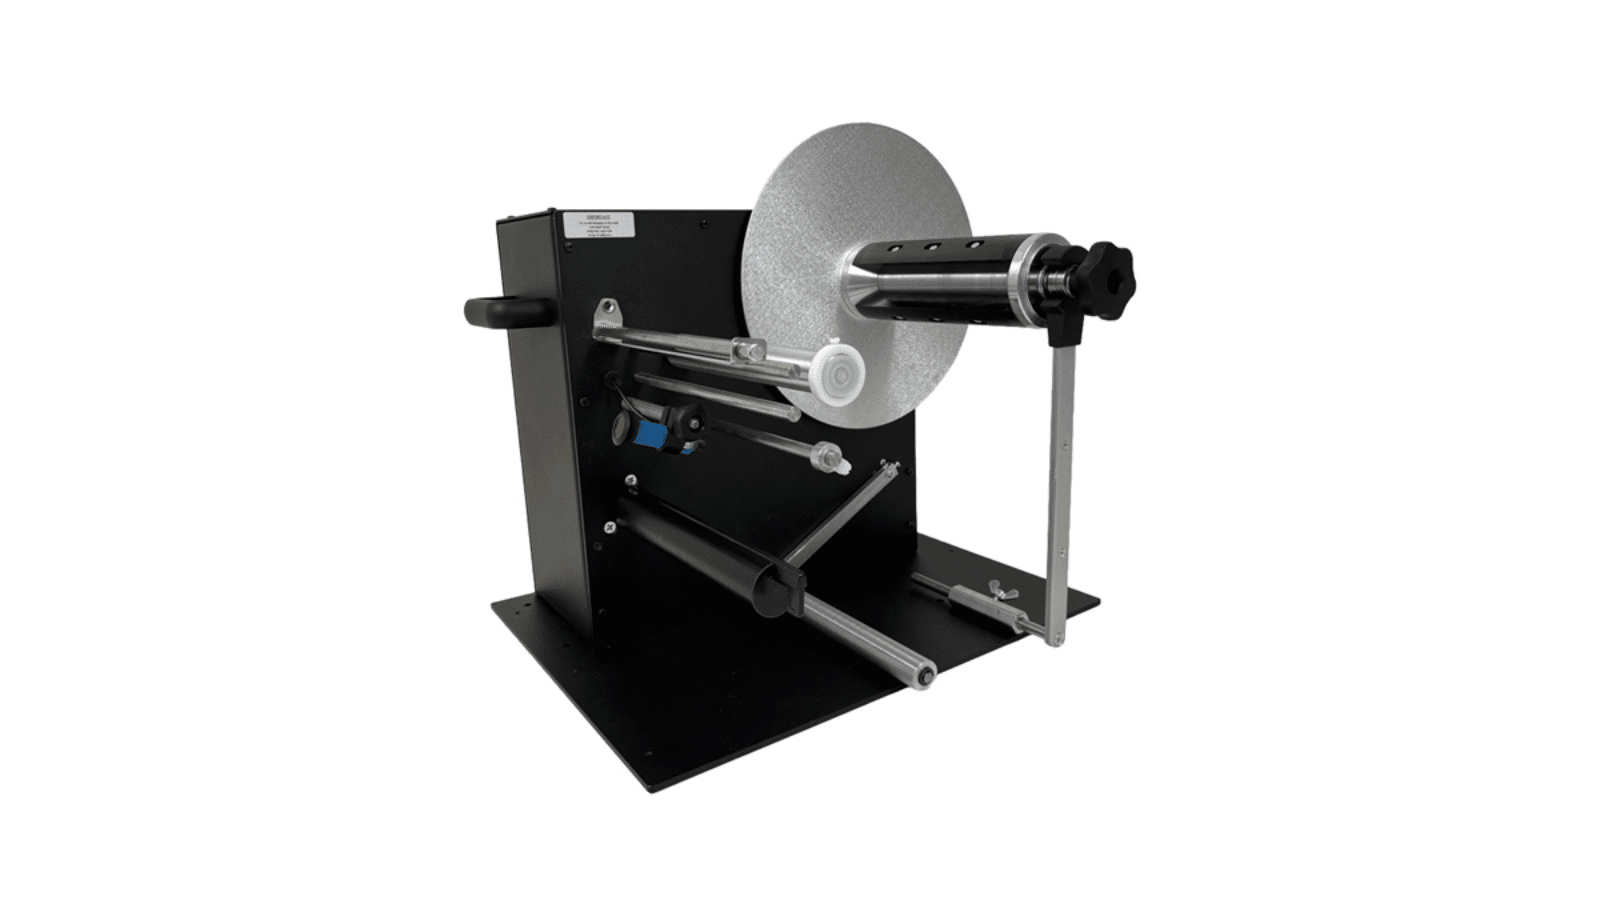
Labelmate LD-300-UNI
Heavy rolls up to 10 kg
The Labelmate LD-300-UNI smoothly handles heavy label rolls up to 10 kg and 350 mm in diameter with a dual motor for intensive use.
Fast peel-and-present operation
Automatic dispensing with an optoelectronic sensor; the next label is ready after picking up the previous one.
Long warranty
Three years on parts and labor for reliable performance.